
Engineering Excellence in Chemical Storage, Mixing, and Distribution
From conceptual design to final fabrication, R.M. Technologies of America provides high-performance infrastructure for industrial chemical applications. We specialize in safe, reliable, and compliant systems for the following chemical categories:
Anhydrous Ammonia (NH₃) Systems
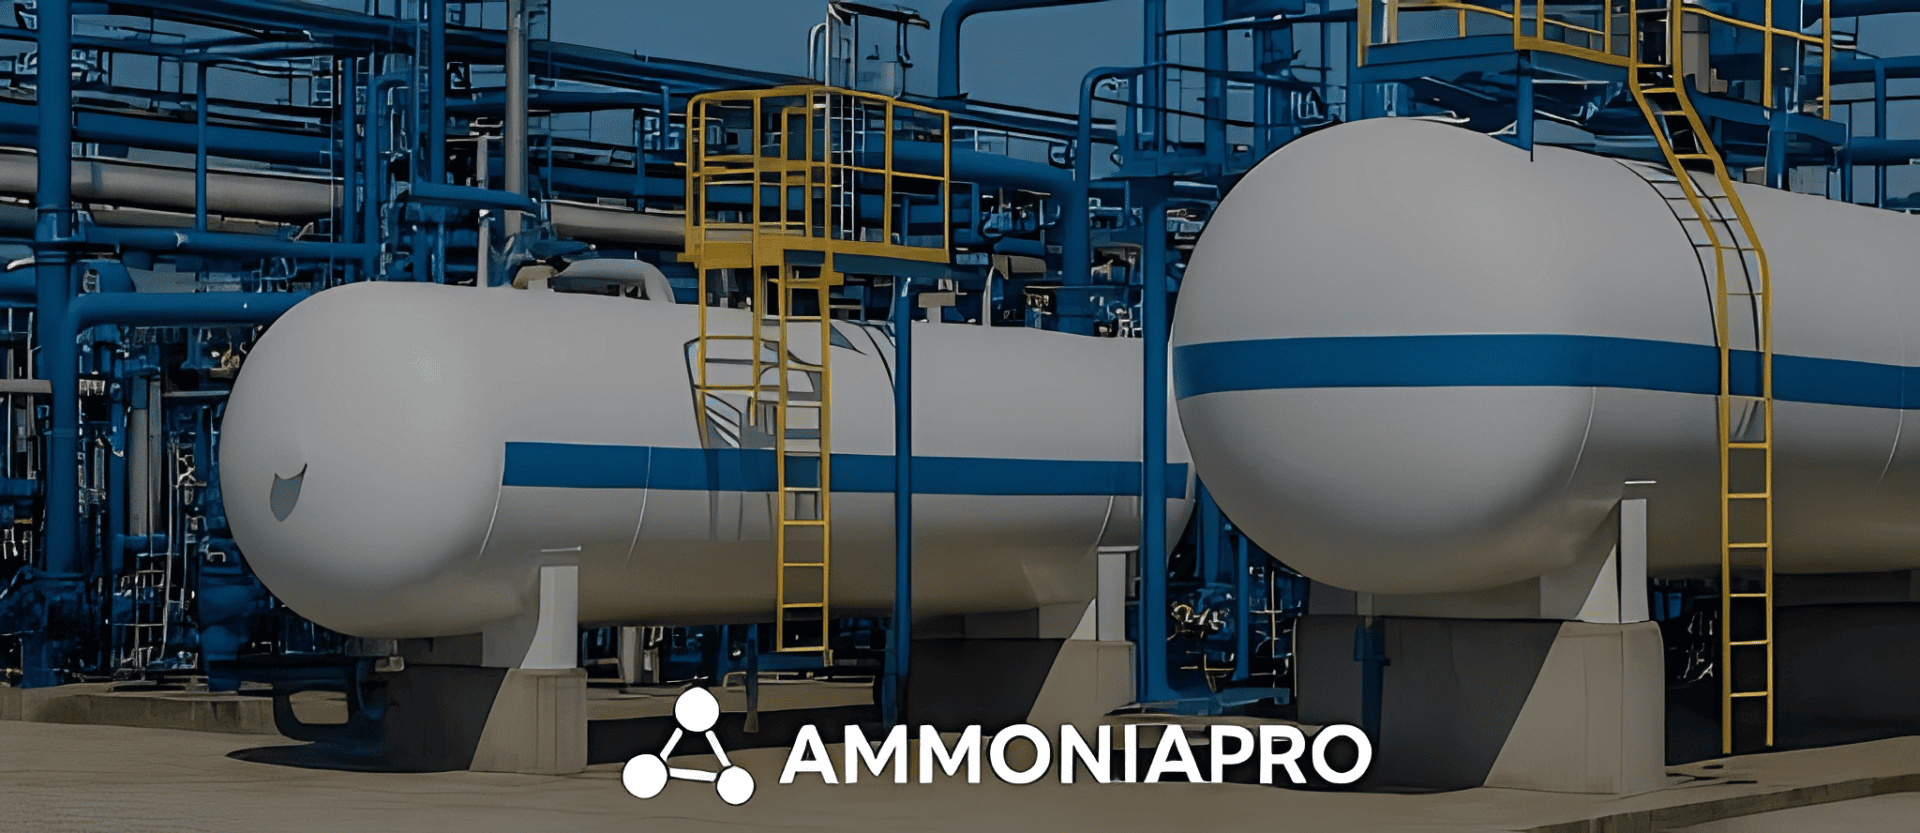
Integrated storage and distribution solutions designed for high-pressure safety and precision.
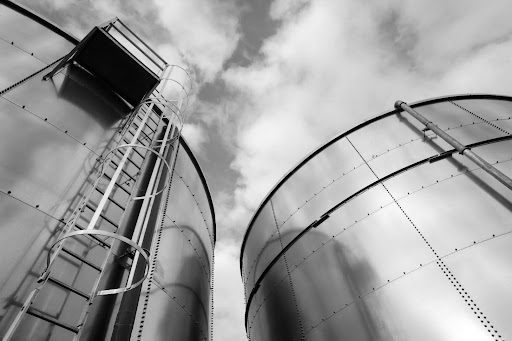
- ASME Storage Tanks: Certified high-pressure vessels for secure chemical containment.
- Ammonia Vaporizers: Efficient conversion systems for process-ready gas delivery.
- Pump Skids: High-reliability transfer and circulation modules.
- Unloading Skids: Dedicated stations for safe Truck and Railcar intake.
- Dilution Fan/Blower Skids: Specialized air-mixing systems for concentration control.
- Safety & Monitoring: High-sensitivity Ammonia Detectors and integrated Scrubber systems.
Consult with a Systems Engineer
Get technical insights on your ammonia system design, fabrication, or regulatory compliance needs.
"*" indicates required fields

Ammonium Hydroxide (Aqua Ammonia) Systems
Engineered integration and delivery systems for controlled aqueous chemical processing.
- ASME Storage Tanks:Specialized vessels tailored for Ammonium Hydroxide (NH4OH).
- Mixing & Production Skids:On-site blending systems for precise chemical concentrations.
- Vaporizers & Pump Skids:Robust components for efficient fluid handling and conversion.
- Truck Unloading Skids:Streamlined intake systems for bulk liquid delivery.
- Dilution & Scrubbing:Advanced Fan/Blower skids and emission-controlling Ammonia Scrubbers.
- Detection Systems:Continuous monitoring for enhanced facility safety.
Urea Systems [CO(NH2)2]
Operational performance solutions for accurate dosing and stable handling.
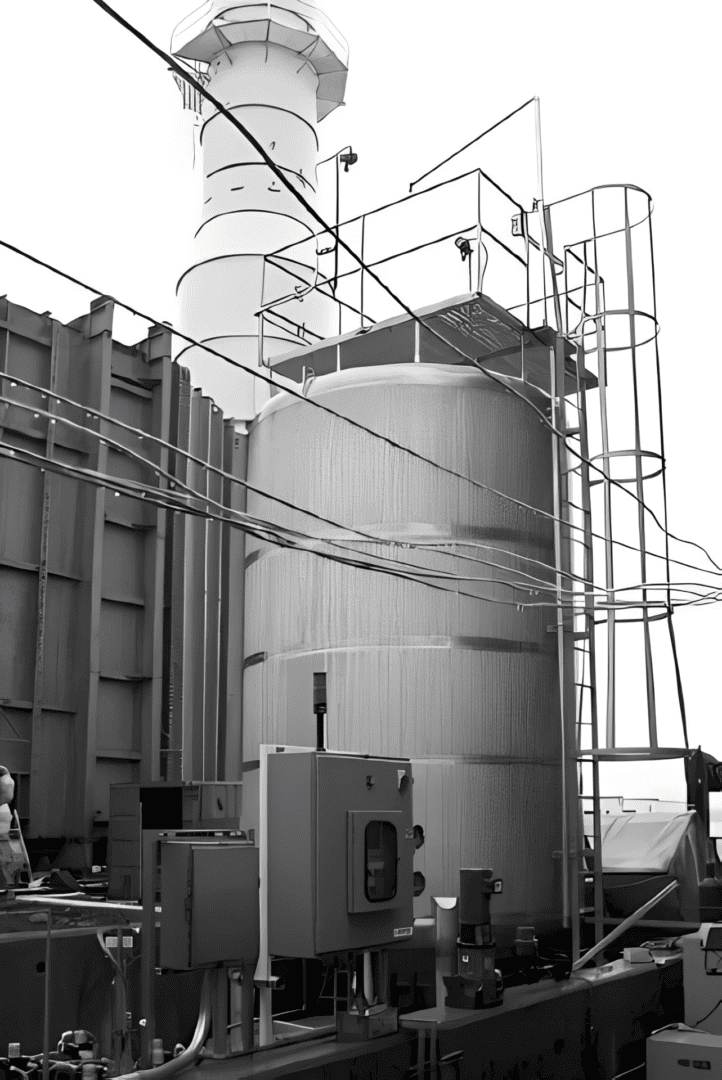
- Urea ASME Tanks:Durable storage solutions engineered for long-term stability.
- Mixing & Production Skids:Custom-built modules for urea solution preparation.
- Pump & Unloading Skids:Reliable hardware for consistent fluid transfer and bulk delivery.
- Dilution Fan/Blower Skids:Precision air-flow management for chemical dilution.
- Environmental Protection: Integrated Ammonia Scrubbers and Detection hardware.
Ammonium Carbonate Systems [(NH4)2CO3]
Specialized infrastructure for stable storage and smooth transfer operations.
- Ammonium Carbonate ASME Tanks:Regulated storage vessels for chemical integrity.
- Mixing & Production Skids:Automated blending solutions for process consistency.
- Pump Skids:High-efficiency transfer modules for downstream delivery.
- Facility Safety:Industrial-grade Ammonia Detectors and specialized Scrubbing systems.